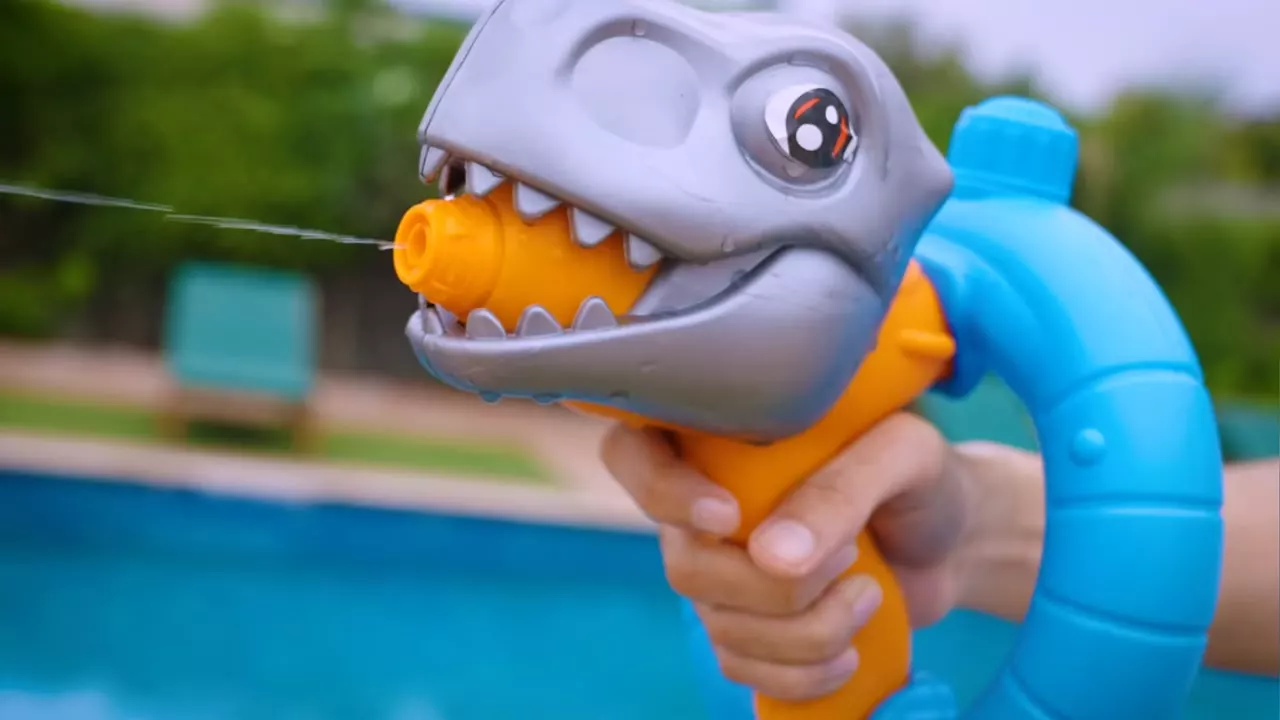
Factory direct · Made in India
Water guns, manufactured in India
A summer toy. Water play runs every year in every market we ship to. Our own injection and blow moulding, made to ASTM and EN-71, with certificates issued per shipment.
- Manufacturing since
- 1951
- People
- 1,200+
- The floor
- 3 presses · 2 blow lines
- Toy safety
- ASTM F963 · EN-71
- Ships to
- 5+ countries
This supplier
What you are buying from
A named manufacturer
One company, our own plants, a registered name and a floor you can visit or have audited. Guns are moulded, assembled, tested and packed at Faridabad, and you deal with the people who run it.
Both moulding processes under one roof
Injection for the mechanism, blow moulding for the reservoir. A gun with a large tank and a fine pump is made as one product here.
Made in India
A second country of origin in a category most buyers source from one, for anyone diversifying supply or watching tariff exposure on a single lane.
Certificates issued per shipment
Issued against your consignment. Raise a national scheme at enquiry and it is settled before tooling runs.
The range
Three size classes
Materials, dimensions and carton configuration are confirmed against your SKU at quotation. What the floor sustains for each class is in the next section.
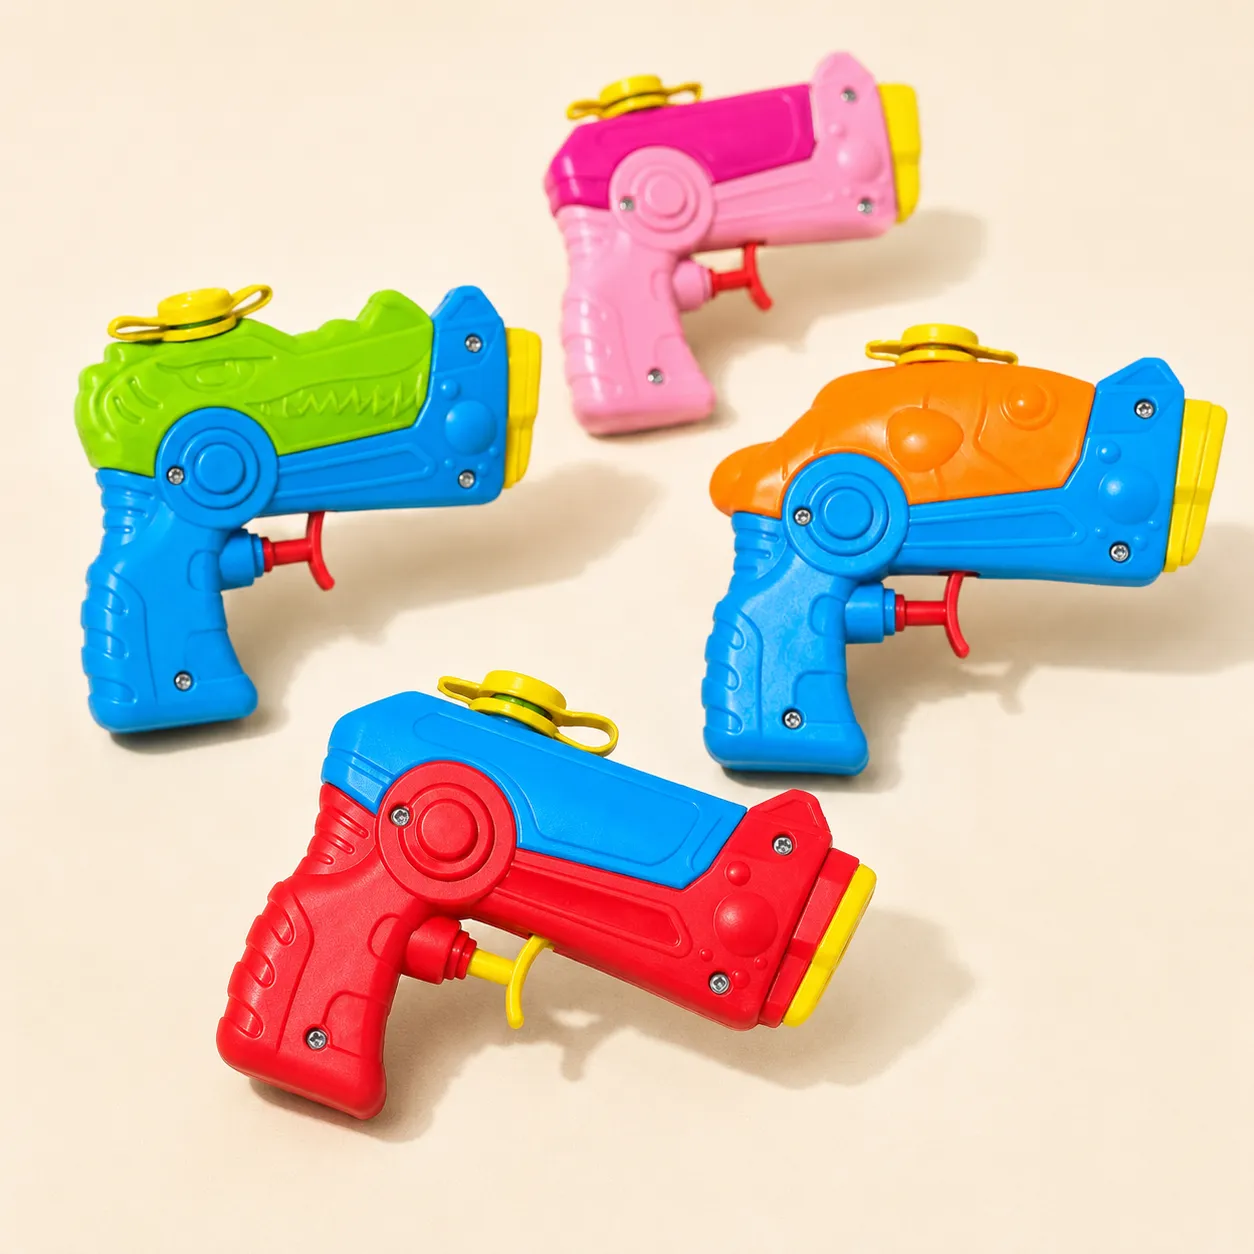
Pocket squirt
The impulse and pocket-money end. Single-piece body, simple plunger, sold in multipacks and on clip strips.
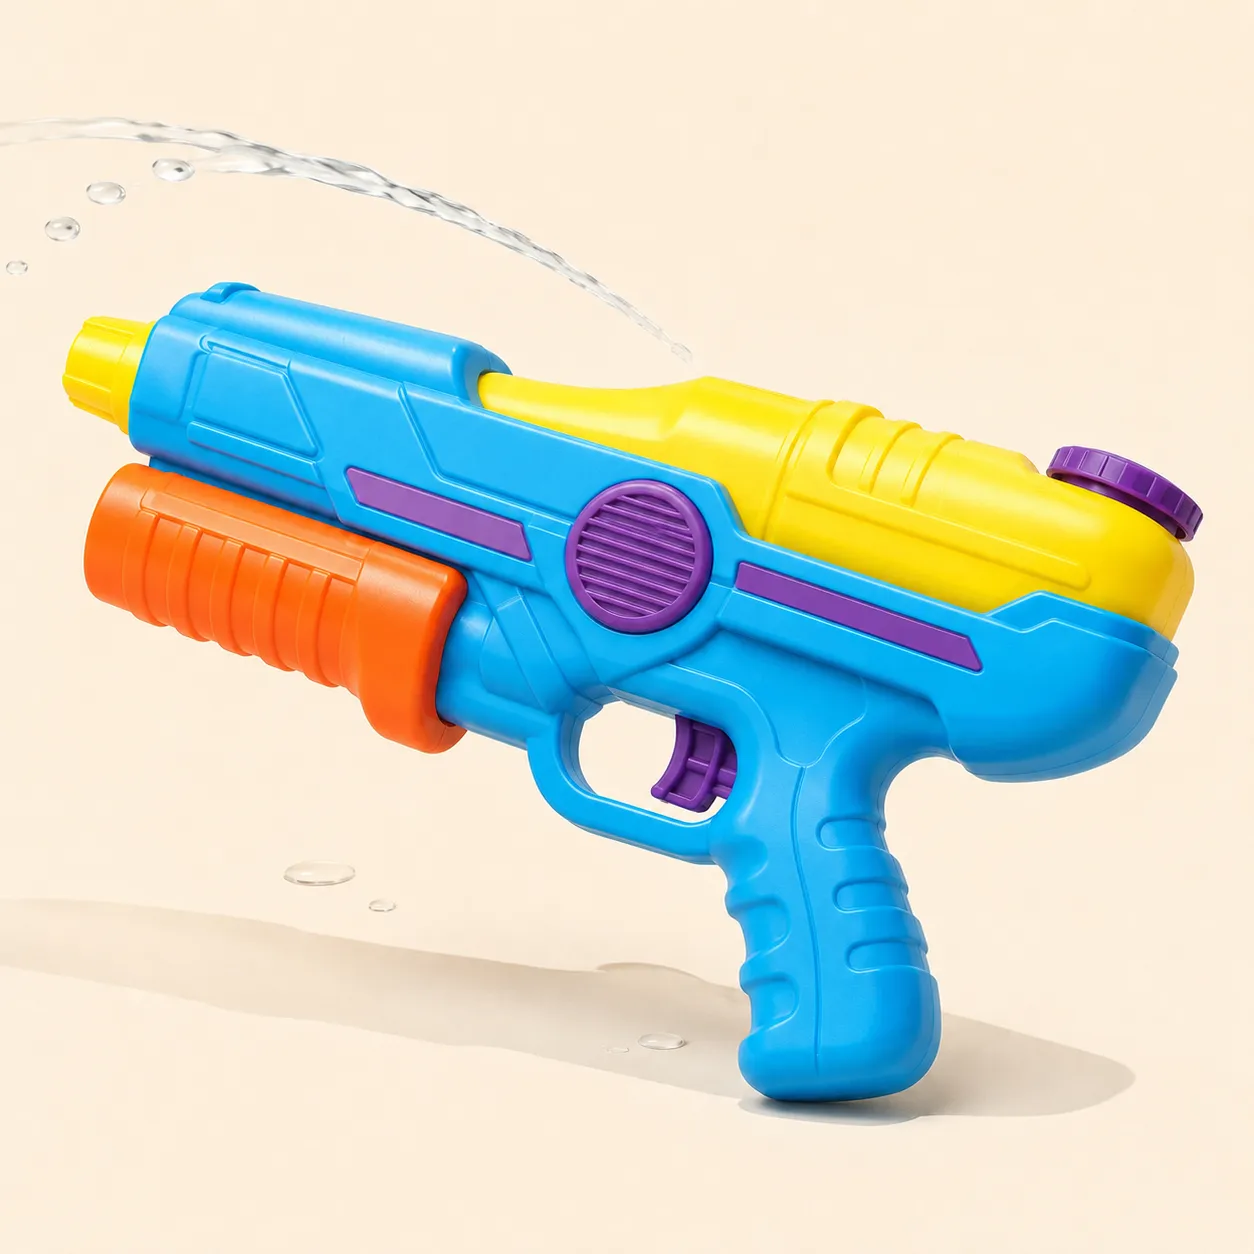
Mid pump-action
The volume seller. One-hand pump, moulded reservoir, the size class most seasonal toy aisles build the shelf around.
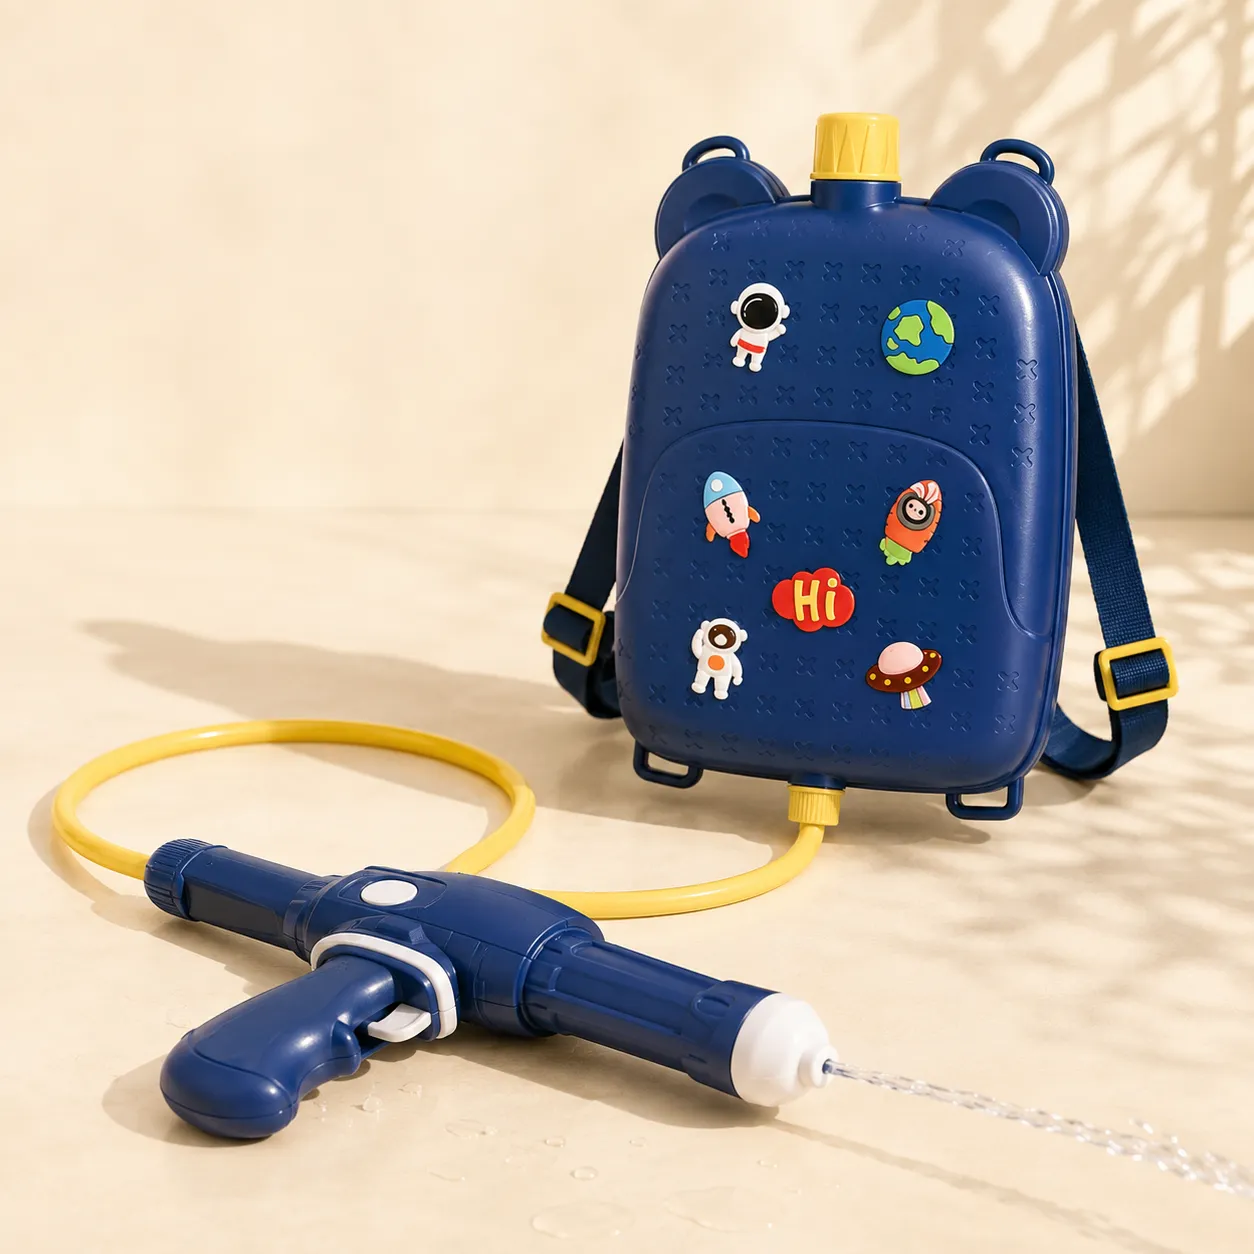
Backpack tank
Worn reservoir with a hose and lance. The top of the range, the slowest to make by design, and the clearest demonstration of both moulding processes in one product.
Capacity
One floor, one pool
Everything on this page comes off one shared moulding and assembly floor: three injection presses and two blow-moulding lines, run on two shifts at roughly 18 to 20 running hours a day.
That matters because our capacity is a single pool. The presses, the assembly benches and the QC stations that make a pocket squirt are the same ones that make a backpack tank, so the size classes share it. The rates here are continuous-running rates the floor holds month after month.
- Pocket squirt
- about 800,000 a month
- Single-piece body, simple plunger. The fastest thing the floor makes.
- Mid pump-action
- about 400,000 a month
- A pump, a moulded reservoir and more parts to stage and assemble.
- Backpack tank
- 100,000 to 300,000 a month
- Two mouldings from two machines at once, straps, screws and seals, a longer ultrasonic seal and a larger vessel to water-test. One backpack takes several squirts' worth of line time.
These are the rates for a floor set to one class. The figure for an order is worked from its size-class split.
The floor
How a gun crosses the floor
Every gun, whatever its class, moves through the same eight steps and the same three inspection gates, on a floor you can visit or have audited.

The eight steps, in order
- Step 01Gate 1
Raw material intake
Polymer is tested in house before it enters the process. A batch that fails never reaches a press.
- Step 02
Moulding
Three injection presses for mechanisms, two blow-moulding lines for reservoirs, running two shifts.
- Step 03Gate 2
Moulded parts QC
Every moulded part is checked before it goes anywhere. Short shots, flash and warp stop here.
- Step 04
Sleeve cutting
Internal pipes are cut to length on a sleeve-cutting machine, which is what keeps assembly moving at line speed.
- Step 05
Assembly
Conveyor belts line the units up to the benches. Screws go in on automatic screw-driving tools, all of them, so torque is the same on the first gun and the eight-hundred-thousandth.
- Step 06Gate 3
Water test
Every working unit is filled and fired before it is sealed. A leak or a failed pump is caught while it is still cheap to fix.
- Step 07
Seal, sticker and paint
Screwing or ultrasonic sealing, then decoration. The backpack's larger seal is one reason it runs slower.
- Step 08
Final QC and packing
A last check on the finished product, then cartons to the buyer's plan, palletised and handled to the bay for loading.
How you can buy
Off the range, or off a drawing
The five, and what each means
- OEM manufacturing
- Your design and your tooling decisions, our lines.
- Private label
- Our existing range under your brand. No new mould, fastest route to shelf.
- Design customisation
- Changes short of new tooling: colourways, decoration, pack format.
- Custom development
- Concept to production on our tooling, when you have a product in mind and no drawing yet.
- IP-secure production
- For buyers bringing a design they own. Your tooling, parts and run are kept apart on the floor, under NDA.
Compliance
The standard for your market, on your consignment
Toy safety is the question that stops most first orders. It is easier to settle before tooling than after a container is packed.
If your market runs its own scheme, or your buyer requires a named test house or mark, raise it at enquiry.

- United States
- ASTM F963
- EU and UK
- EN-71 · CE
- US children's product
- CPSIA / CPC
- Issued
- Per shipment, on request
- Third-party inspection
- By arrangement
- Management systems
- ISO 9001 · 14001 · 45001
Loading
These fill a container by volume long before weight
Moulded water guns are mostly air. A container cubes out well before it reaches its weight limit, which means the loading plan is worth more to your landed cost than a lower unit price: how the bodies nest, what goes in the void, whether a mixed load beats a single SKU. We work that plan for each order, and we do the documentation and the loading ourselves.
Process
From enquiry to container
Orders for a northern-hemisphere summer are usually placed between October and January. Earlier is a better slot.
- Ready-made design
- A full container of around 400,000 pieces ships in roughly one month and ten days, subject to the sales orders already booked ahead of yours.
- New custom product
- Design runs two to three weeks. Tooling is ready in about two to two and a half months. Delivery then follows the complexity of the piece.
01
Enquiry
Market, size classes, indicative volume and the certification required. A quotation is worked from those four.
02
Sample and spec alignment
Samples against your reference, pack format agreed, any national scheme settled before tooling runs.
03
Production slot
Your order is allocated a share of the pool against your delivery window, behind the orders already booked. Northern-hemisphere summer sits in the quieter half of our year.
04
QC and loading
Checks during the run, third-party inspection if you want it, then loading and documentation from our own bay.
Request a quote
The order
Market, size-class split and delivery window. The order is allocated its share of the pool against those, and the date it is given is the date it ships.
- +918755209308
- The company
- Garg Global Innovative Limited. Who we are and how we make it.